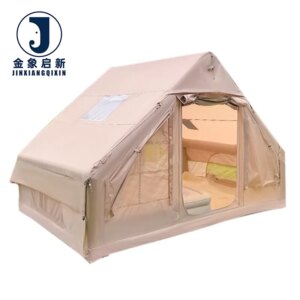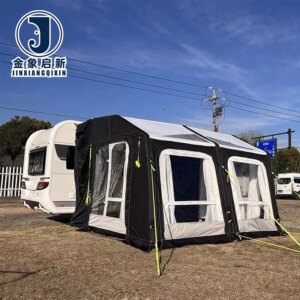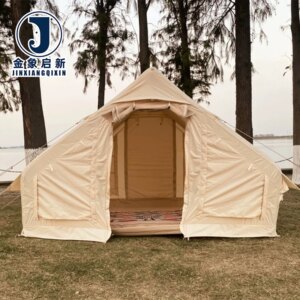
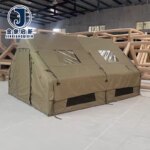
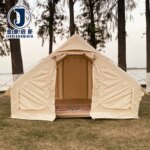
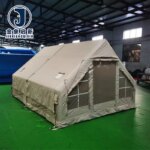
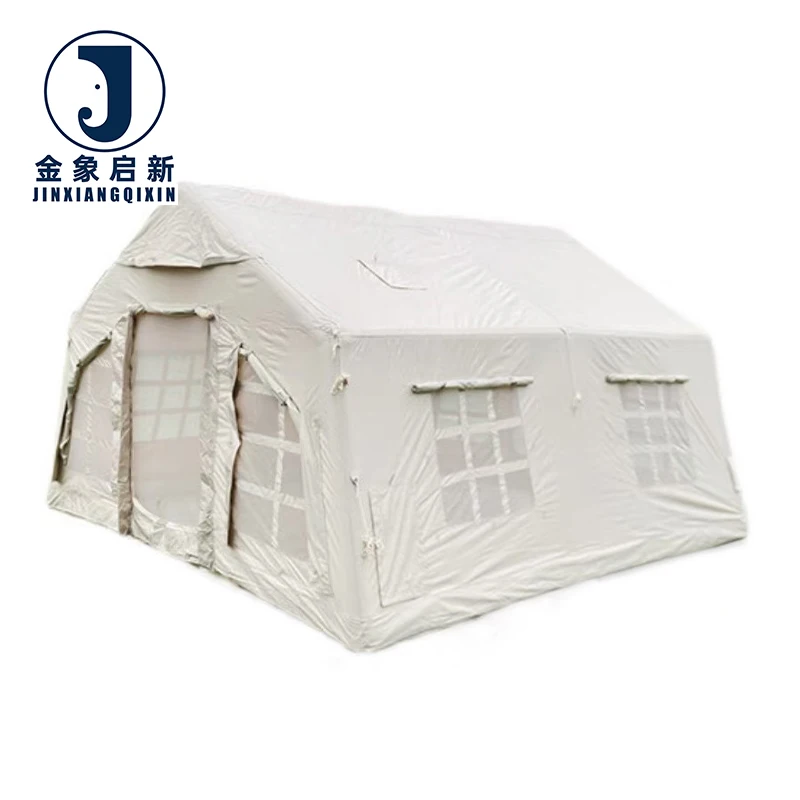
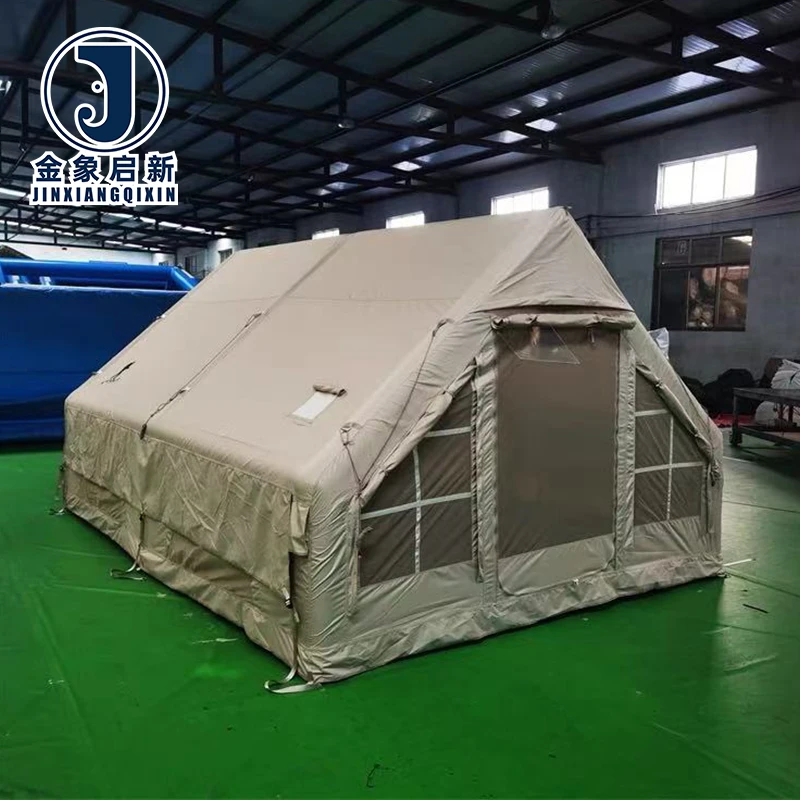
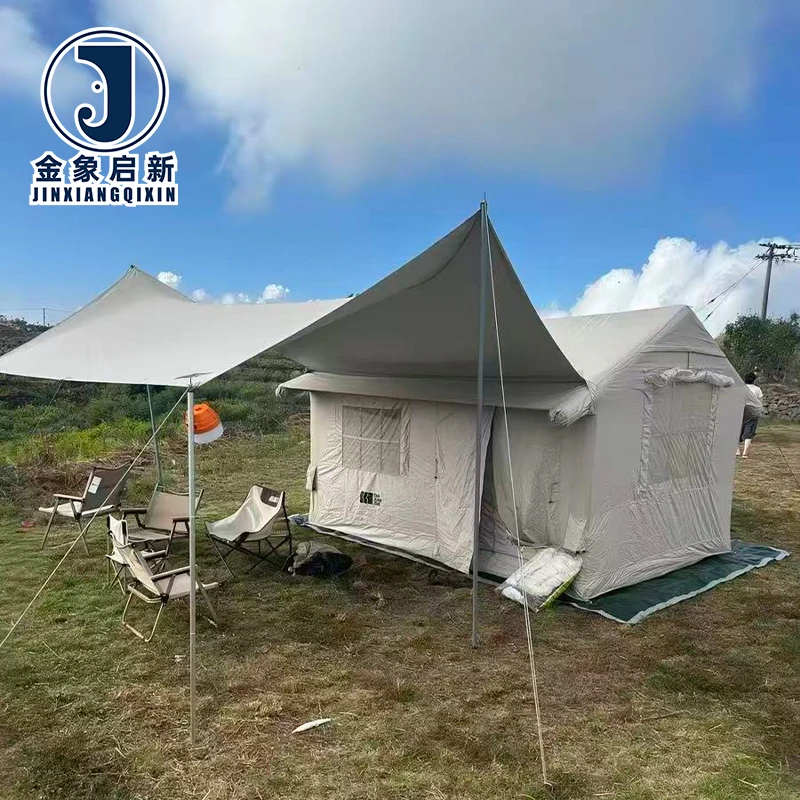
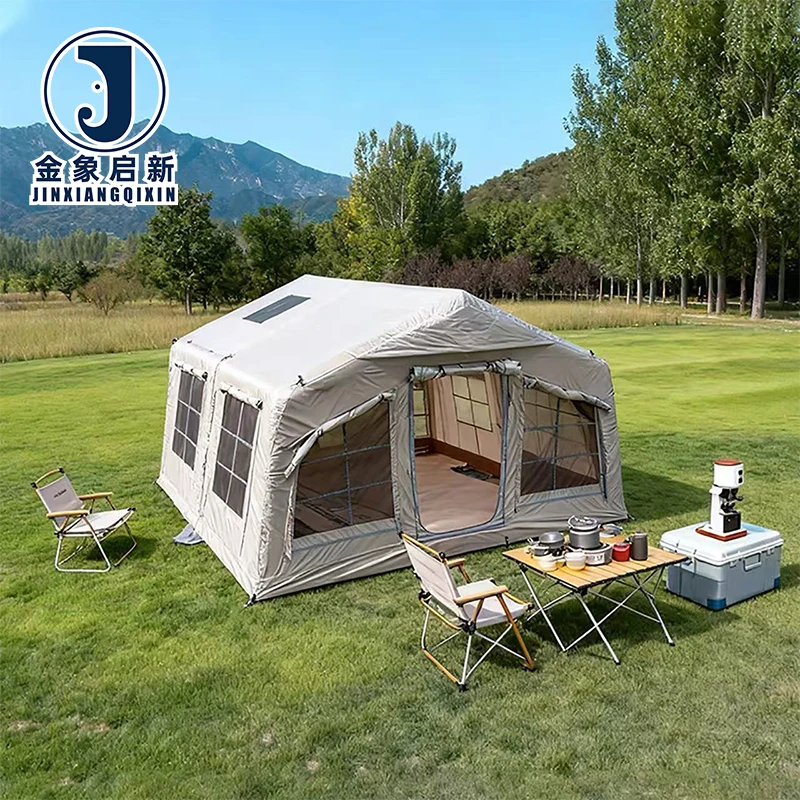
Proven Process Control — Three full production lines and 36 sets of specialist equipment enable consistent coating weight and adhesion across every roll of inflatable structure fabric we produce.
Technical Specifications
| Parameter | Value |
|---|---|
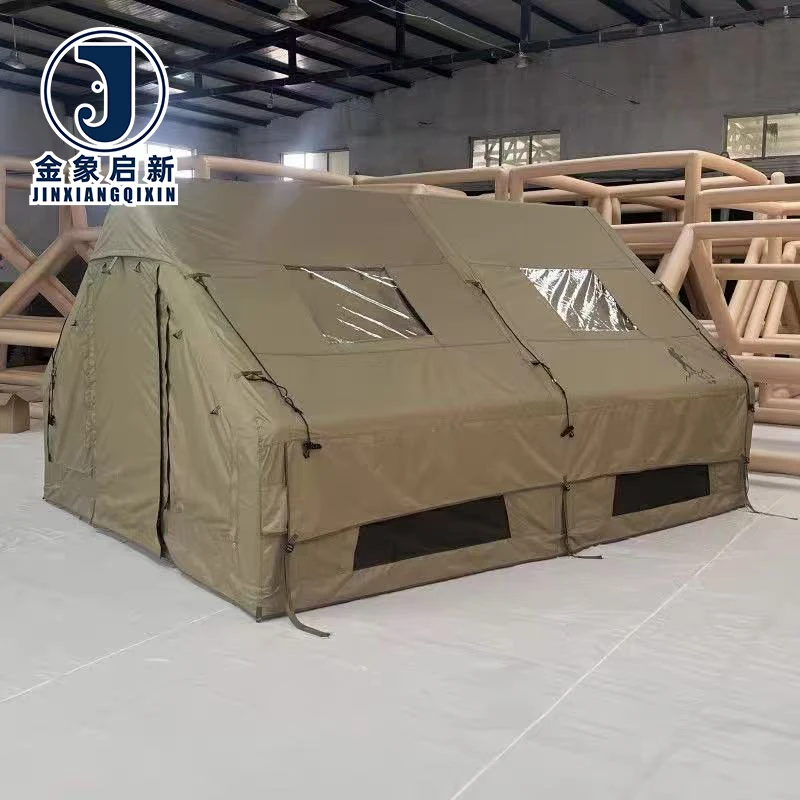
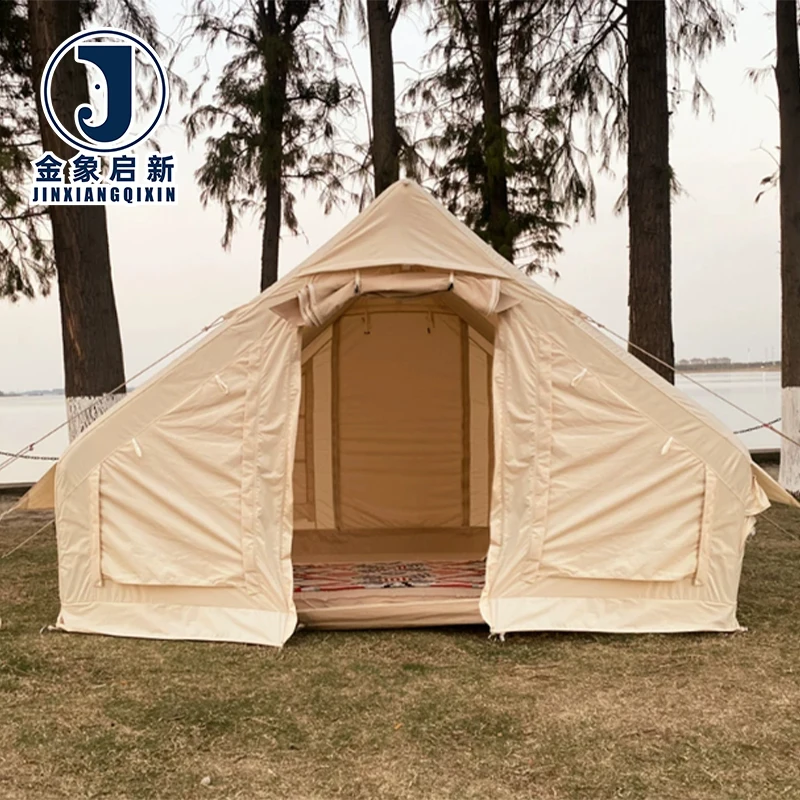
| Product Type | Inflatable tent |
| Core Material | PVC Tarpaulin |
| Key Performance | Waterproof, Tear-resistant |
| UV Resistance | Available with UV treatment — test basis not stated in source, confirm grade required for your market |
| Fire Retardancy | Available in fire-retardant grades — confirm the grade required for your market |
| Anti-Static | Available with anti-static treatment — confirm the surface resistance standard applicable to your site |
| Capacity | 4–6 Person |
| Construction | Single layer |
| Opening Mechanism | Quick automatic opening |
| Customization | OEM & ODM, sample customization, pattern printing |
| R&D Support | 10 technicians handling material selection and sample development |
| Quality System | Full-process inspection with dedicated QA & QC staff |
| Standards | ISO 9001, ISO 14001, ISO 45001, CE |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Inflatable membrane structures | Continuous UV and weather exposure, structural air-pressure load, fire-code compliance for public assembly |
| Mining ventilation ducting | Abrasive particulate, flame-spread limitation, anti-static surface to prevent ignition in explosive atmospheres |
| Aviation ground-support ducts | Jet-fuel residue contact, rapid deployment and retrieval, fire-retardant certification for airside use |
| Tunnelling ventilation | High humidity, rock-dust abrasion, fire-retardant and anti-static compliance for underground safety regulations |
| Temporary event shelters | Frequent inflation-deflation cycles, crowd-proximity fire safety, transport abrasion during logistics |
What "Certified Fabric" Means When the Certificate Is Missing
Specifying inflatable tent fabric fire retardant certified without verifying the test report is a compliance risk, not a procurement saving.
Commercial operators and specialist contractors often receive inflatable structures or ventilation ducts that carry a fire-retardant claim on the invoice but arrive with no underlying test documentation. When a site inspector or safety auditor asks for the grade, the supplier chain stalls. [NEED_CITE: fire classification standards for inflatable and temporary structures vary by jurisdiction] The result is delayed project handover, rejected shipments, or — worst case — a structure operating without the fire performance its occupants assume it has. We see this pattern repeatedly in mining, aviation and large-scale event applications where the inflatable tent aftermarket supplier is expected to provide not just fabric, but the documentation that proves the fabric meets the site’s mandatory standard.
Ventilation and Membrane Fabric Built for Technical Compliance
The inflatable tent fabric fire retardant certified range is engineered for applications where the material must satisfy both mechanical and regulatory demands simultaneously. PVC tarpaulin forms the base, providing waterproof and tear-resistant performance through a single-layer construction that balances air-holding integrity with transport weight. Each roll or finished unit moves through a quality system staffed by dedicated QA and QC personnel, ensuring that coating adhesion and base-fabric alignment are verified before the material leaves the line.
How Fire-Retardant and Anti-Static Options Are Integrated
Fire-retardant and anti-static treatments are incorporated during the coating stage rather than applied as an after-market finish, which preserves the fabric’s flexibility and weld integrity. [NEED_CITE: DIN 4102 fire classification for building materials and temporary structures] Because compliance requirements differ between an Australian underground mine, a European event venue and a Middle-East aviation hangar, we confirm the exact grade and surface-resistance standard with the buyer before production starts. This prevents the common situation where fabric arrives certified to a standard the local authority does not recognise.
Reading the Specifications Beyond the Headline Claims
GSM alone does not predict how an inflatable membrane will behave under sustained air pressure or cyclic inflation. Base-fabric denier and weave density work together with coating weight to determine tensile and tear behaviour; a heavier coat over a loosely woven base may resist puncture but can delaminate at the weld line when the structure flexes. The PVC coating method — whether knife-over-roll, dip, or calender — directly influences peel strength and therefore the temperature window available for hot-air welding on site. Single-layer construction reduces packed volume and weight, an advantage for contractors shipping duct sections or event shelters to remote sites, but it also places the entire structural and environmental load on one composite. Understanding these relationships helps buyers specify inflatable tent aftermarket supplier requirements that match real field conditions rather than brochure values.
The Hidden Cost of Specifying on Price Per Roll Alone
When procurement decisions rest on quoted GSM without a verification step, the delivered fabric can arrive lighter than agreed — a shortfall invisible until the material fails prematurely at stress points. Fire-retardant claims unsupported by a test report leave the buyer holding an uninsurable structure. Batch-to-batch colour drift across a multi-roll order becomes obvious only after panels are welded side by side on a membrane facade. [NEED_CITE: tensile and tear test methods for coated fabrics per ISO 1421] Welded seams that fail before the fabric itself does are frequently traced to coating-weight inconsistency that altered the heat-seal window mid-production. These are not rare events; they are recurring patterns we encounter when contractors switch to an unverified inflatable tent aftermarket supplier to save a percentage point on unit cost.
Why Technical Buyers Source This Fabric Here
Our 10-technician R&D team handles material selection, pattern printing and sample development in-house, so custom widths and fire-retardant grades are confirmed before mass production begins, not discovered as a problem afterward. Three full production lines and 36 sets of specialist coating and welding equipment provide the capacity to hold delivery dates on bulk ventilation-duct orders without subcontracting critical stages. A dedicated QA and QC function inspects every roll before shipment, catching coating-weight variance and colour drift that would otherwise surface on the job site. ISO 9001, ISO 14001, ISO 45001 and CE certifications are maintained not as wall plaques but as operating frameworks that shape how we document and trace each batch. Sample development is completed within days for custom inflatable structure requirements, giving buyers a physical reference to test weld parameters and confirm compliance before committing to volume.
Documentation & Verification
- Material specification sheet confirming PVC base fabric, coating type, and weight parameters for each roll
- Fire-retardant test report matching the grade specified on the purchase order, issued per batch
- Anti-static surface-resistance test result where applicable to mining or aviation site requirements
- Pre-shipment inspection record covering coating adhesion, dimensional accuracy, and visual consistency
- ISO 9001, ISO 14001, ISO 45001 and CE certificates available for supply-chain audit submission
- Certificate of origin and customs documentation package for international inflatable structure shipments
Fabrication, Handling & Storage
- Hot-air weld temperature and speed must be calibrated to the specific PVC coating weight of this single-layer fabric
- Store rolls upright on end-caps to prevent permanent creasing that weakens the coating at fold lines
- Allow cold-stored rolls to acclimatise to workshop temperature before unrolling to avoid surface micro-cracking
- Use PVC-compatible cleaners only; solvent-based products can degrade the coating bond on this tarpaulin
- Plan panel cutting layout to minimise transverse welds, reducing potential leak paths in inflated structures
- Repair minor field punctures with compatible PVC patch kits heat-welded, not adhesive-bonded, to maintain air integrity
Before You Request a Quote
Provide the end-use application — whether inflatable membrane, ventilation duct, or temporary shelter — along with the fire-retardant or anti-static grade your local authority requires. Specify target dimensions, annual volume, and whether you need finished units or roll stock for your own fabrication line. If colour matching or pattern printing is part of the project, share the reference standard so our R&D team can prepare a physical sample before you commit to production.
Frequently Asked Questions
Q: What fire-retardant grades are available for inflatable structures?
A: We supply fabric in multiple fire-retardant grades aligned to standards such as M2, B1, and NFPA 701. The exact grade available depends on the coating formulation selected for your application. Confirm the standard mandated by your local authority or project specification, and we will match the formulation and provide the corresponding test report with your shipment.
Q: How is anti-static performance verified and what standard applies?
A: Anti-static performance is measured by surface resistivity testing on the finished coated fabric. The applicable standard depends on whether the duct or structure operates in a mining, tunnelling, or aviation environment. Share your site’s required surface-resistance range, and we will formulate the coating accordingly and include the test result in your batch documentation package.
Q: What documentation ships with each batch to meet site compliance?
A: Every shipment includes a material specification sheet, the relevant fire-retardant or anti-static test report, a pre-shipment inspection record, and certificates of ISO and CE compliance. For international orders we also provide a certificate of origin and full customs documentation. Mining and tunnelling contractors typically require the complete set for safety-audit submission.
Q: How are custom dimensions and OEM samples handled before mass production?
A: Our 10-technician R&D team develops physical samples covering custom size, coating weight, and pattern printing within days of receiving your specification. You evaluate the sample for weld behaviour, colour accuracy, and compliance alignment before approving mass production. This step prevents costly mismatches between your engineering requirement and the delivered roll stock.
Q: What process ensures colour and coating consistency across large orders?
A: Each production run follows a controlled coating process with in-line QA checks on weight and adhesion. Dedicated QC staff compare every roll against the approved colour standard and specification sheet before packing. Batch-level inspection records accompany the shipment, giving you documented proof of consistency across your entire order volume.